In the Saratov region, a large-scale project is being implemented to develop dairy farming and milk processing, with the ultimate goal of creating a modern cheese production facility. Investors and local authorities are confident that this new complex will significantly contribute to providing the region with high-quality dairy products and create new job opportunities.
Over the past four years, the farm has carried out tremendous work to modernize and expand its production base. A modern farm has been built to accommodate 1,040 head of cattle, as well as a calf house for 360 young cattle. This has significantly increased the number of animals and created optimal conditions for their care.
The introduction of advanced technologies is a key aspect of the farm's development. The farm has four Lely robots that automate the milking process, ensuring high-quality milk and reducing the dependence on human factors. Additionally, 255 Ayrshire heifers, known for their high productivity and milk quality, have been imported. The result has been the birth of 103 calves this year, indicating the successful adaptation and fertility of the new herd.
Currently, active construction of new facilities is underway. Modern barns that meet the latest zootechnical requirements are being built, as well as a feed mill that will provide the animals with balanced and nutritious feed of their own production. This will allow for the control of feed quality and reduce the cost of purchasing feed.
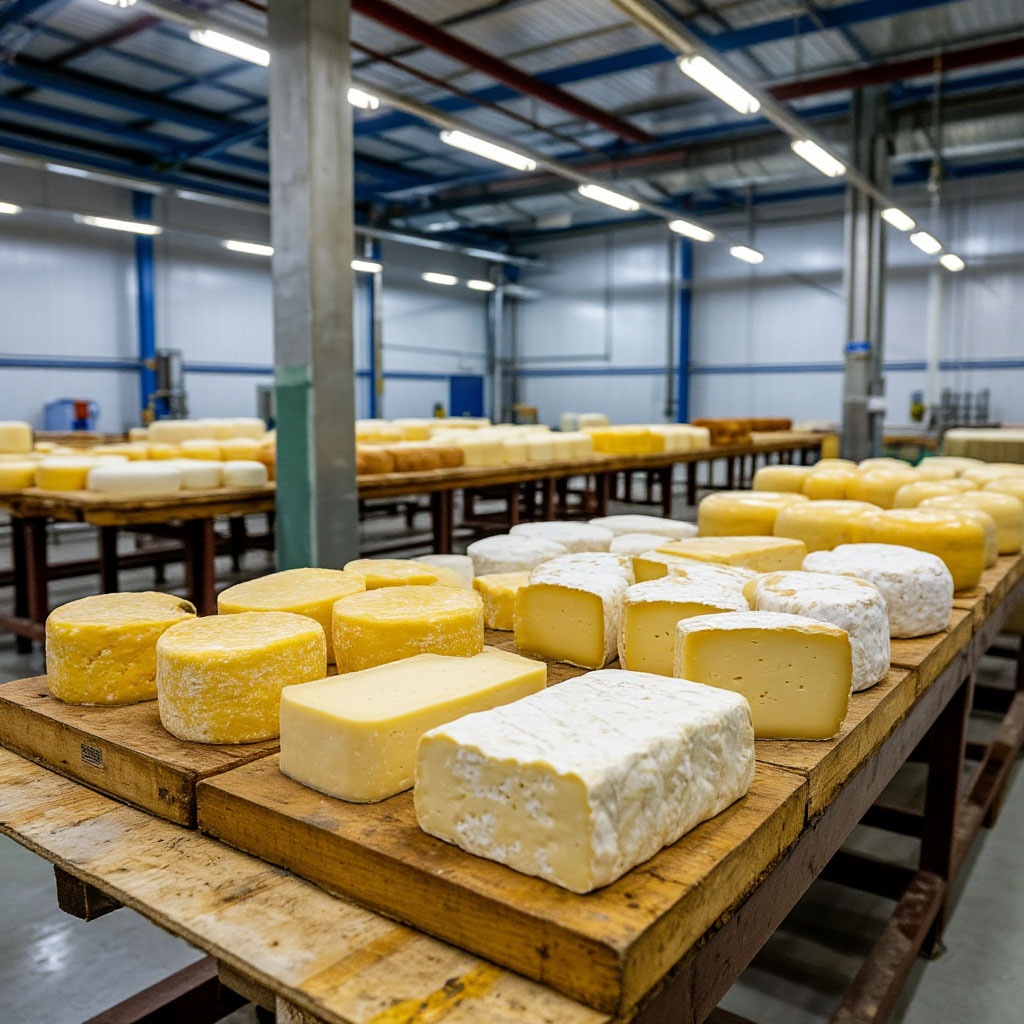
The project will culminate in the launch of a facility for the production of fermented milk products and, most importantly, cheese at the LLC. The processing capacity will be an impressive 4,000 tons of milk per year. This will allow for the production of a wide range of high-quality products, meeting the needs of both the local and regional markets. It is expected that the new production facility will become one of the key suppliers of cheese in the Saratov region, contributing to import substitution and the development of the dairy industry as a whole.
With its extensive experience in the supply and maintenance of industrial refrigeration equipment, AquilonStroyMontazh can become a key partner in the implementation of this ambitious project in the Saratov region. Given the need for specialized refrigeration equipment at every stage of the new production, from raw material storage to finished product maturation, the company is well-positioned to provide comprehensive solutions that meet the highest standards of quality and efficiency.
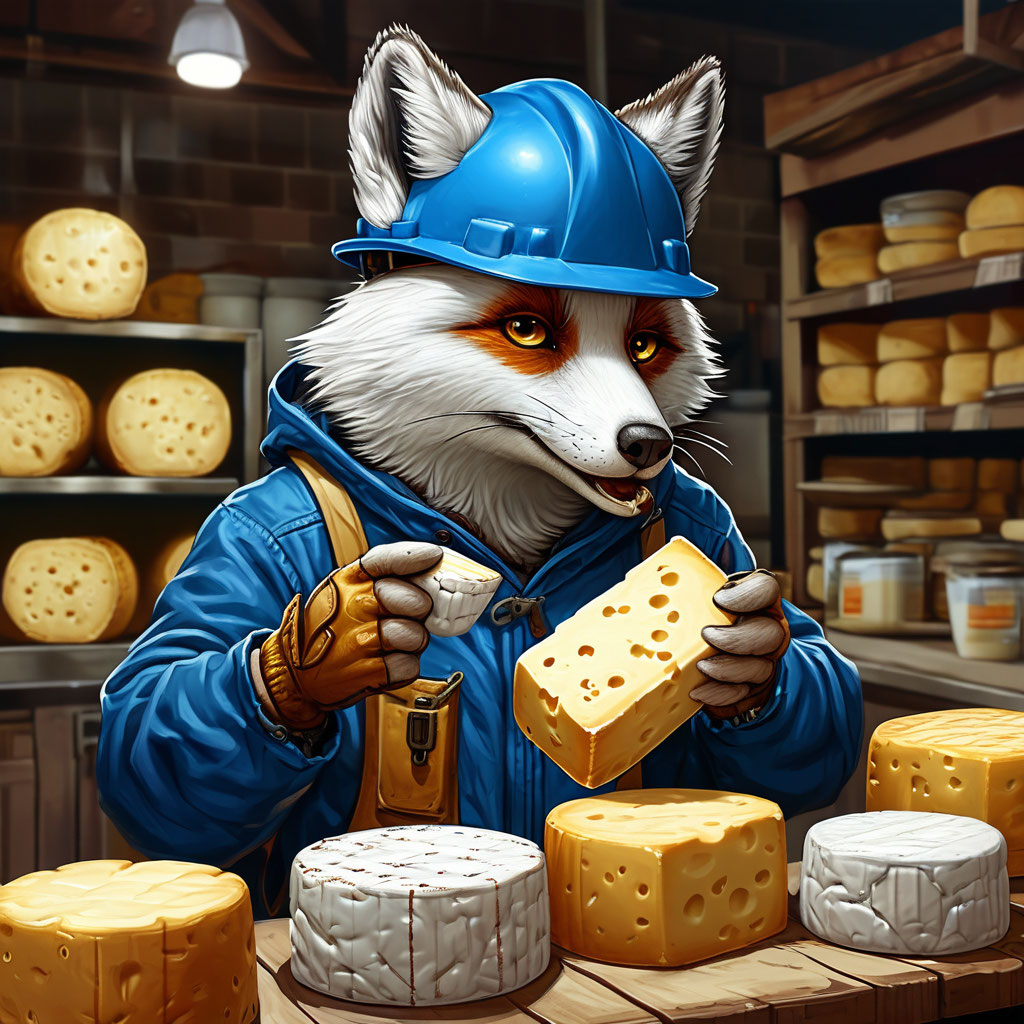
In particular, AquilonStroyMontazh can provide the supply and installation of modern cheese ripening chambers, which guarantee the maintenance of optimal temperature and humidity parameters, which are critical for the formation of the unique taste of each variety. The company can also offer a wide range of tanks for maintaining the required temperature of milk during the curdling process and the production of cheese mass, ensuring the stability of the technological process and the high quality of the final product.
In addition, AquilonStroyMontazh is ready to design and install split systems to maintain the required microclimate in the production rooms where cheese is salted and packaged. This will create comfortable working conditions for the staff and ensure that the products meet sanitary and hygienic standards.
Cooperation with AquilonStroyMontazh will allow the company implementing the project to ensure reliable and uninterrupted operation of all refrigeration equipment, minimize risks associated with temperature violations, and guarantee high-quality products. The company offers not only the supply of equipment, but also a full range of services for its installation, commissioning, service, and repair, which will provide a comprehensive approach to solving the client's problems and ensure long-term stability of the new production facility.
In December 2025, Copeland—a global leader in compressor manufacturing—unveiled a new development: a CO₂ scroll compressor featuring Dynamic Vapor Injection (DVI) technology. This milestone marked a significant step in the evolution of industrial refrigeration equipment, as the combination of the natural refrigerant CO₂ and an advanced vapor injection system opens up new possibilities for enhancing energy efficiency, reducing operating costs, and meeting environmental regulations.
 Выберите размер контейнера: Температурный режим: Новый или Б/У: | Прайс-лист на рефрижераторные контейнеры Вы выбрали: 40 футовые, низкотемпературные, новые 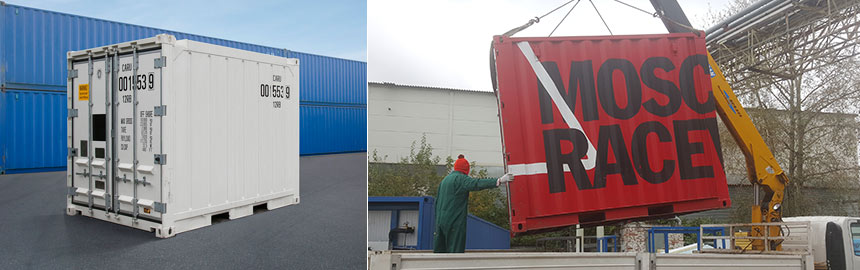
| ||||||||||||||||||||||||||||||||||||||||||||||||||||


 Telegram