These funds are aimed at a deep modernization of the enterprise, including the construction of a new broiler house, the renovation of the slaughter and processing complex, and the re-equipment of existing lines. An important commercial outcome will be the launch of a new product line under the "Vazhnaya Tsypa" brand in 2026. However, behind the facade of these transformations lies a layer of technological changes that directly affect related industrial sectors, particularly the market for professional refrigeration equipment.
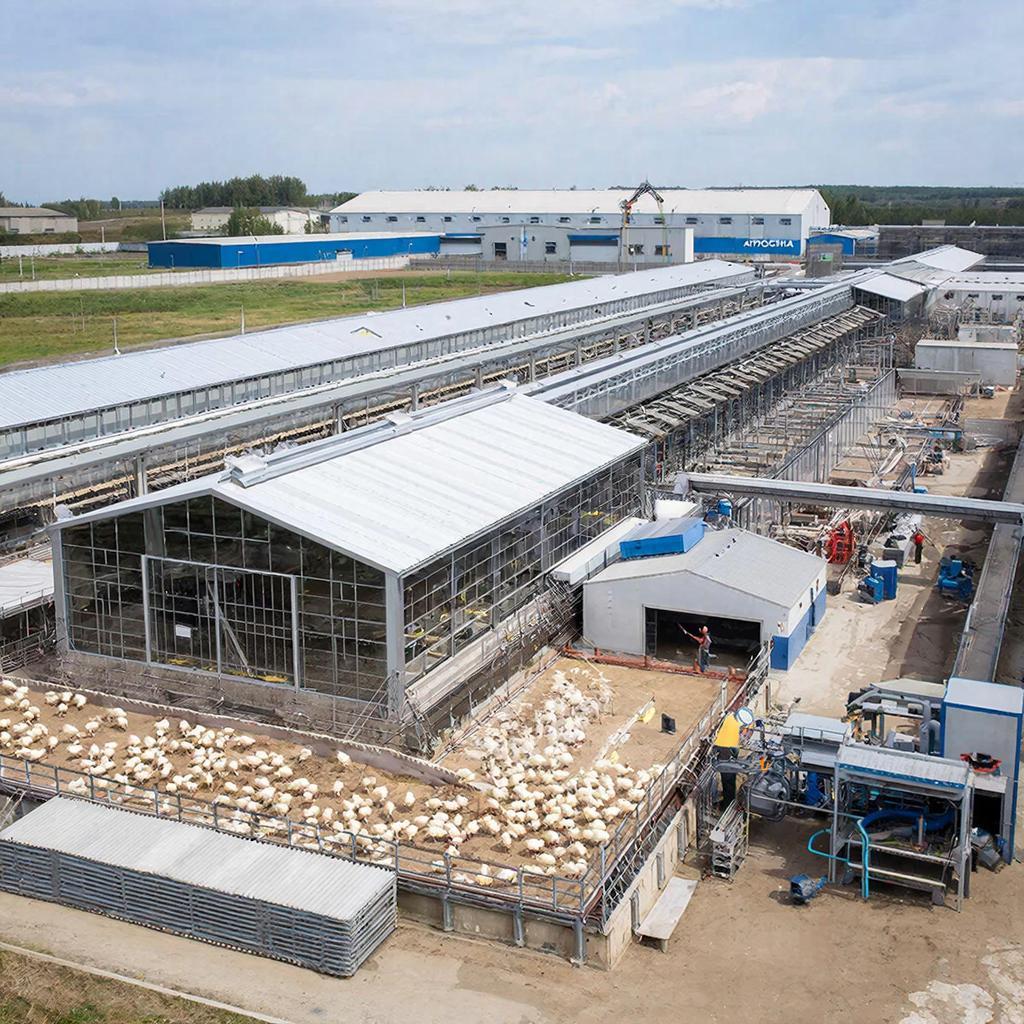
This construction and modernization creates a significant impetus for manufacturers and suppliers of industrial refrigeration solutions. Firstly, the expansion of production capacities, especially in the finished product segment (marinades, cutlets), requires the creation of new refrigeration capacities for storing raw materials and finished products. Secondly, the modernization of the slaughterhouse involves the installation of advanced equipment for cooling and shock freezing of meat, which is a critical step in ensuring safety and quality. Thus, the project generates demand not for individual units, but for complex technological chains, which means large contracts for system integrators in the refrigeration industry.
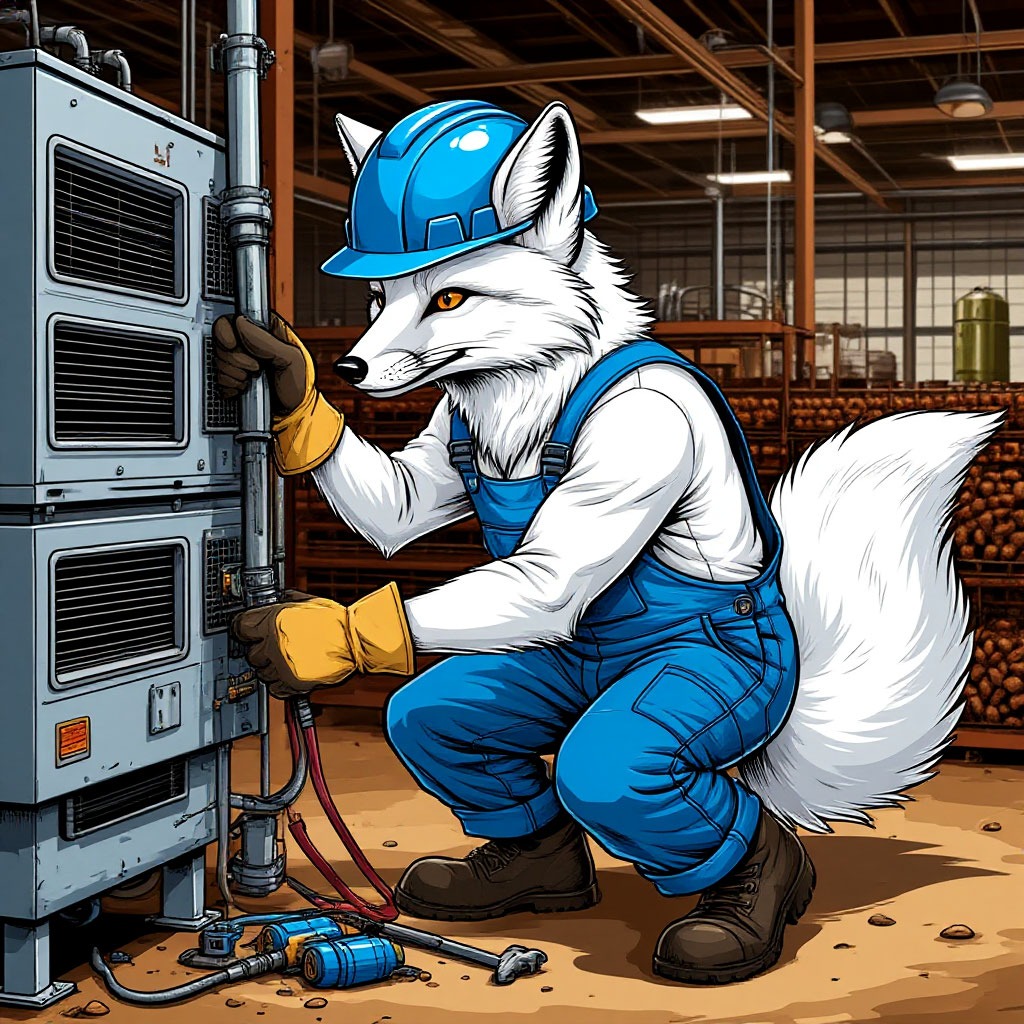
Such projects use a wide range of industrial refrigeration equipment, each component of which performs a strictly defined function.
Industrial refrigeration chambers (refrigerators and freezers). This is the basis of storage logistics. Poultry farms use low-temperature storage chambers (up to -25°C) for long-term storage of frozen carcasses and semi-finished products, as well as cooled storage chambers (from -2°C to +4°C) for short-term storage of chilled meat and ingredients. Key features include large capacity (from hundreds to thousands of cubic meters), energy-efficient insulation, and a reliable automation system for maintaining precise temperature and humidity conditions.
Split systems and chillers for process cooling. They provide cooling for various stages of production. For example, they are used to cool water in technological processes, maintain temperature in marinating rooms, or in packaging rooms. Chillers are centralized refrigeration machines that can cool a heat transfer fluid, which is then distributed to multiple consumers. Their capacity is measured in kilowatts of cold, and the key requirement is to operate smoothly under high load conditions.
Equipment for shock freezing (fluidization tunnels, spiral freezers). This is the most technologically advanced link that directly affects the quality of the product. Shock freezing allows for rapid passage through the critical zone of moisture crystallization in the product, which preserves the cellular structure, taste, and nutritional properties. For cutlets or breaded products, spiral freezers are often used, where the product moves along a conveyor in a stream of air at a temperature of -35°C or lower. Their capacity can reach several tons per hour.
Lamella coolers (air cooling units) for air conditioning and ventilation. They are critical in the production halls themselves, especially in the slaughter and processing areas, where sanitary regulations require maintaining a strictly defined low air temperature (usually no higher than +12°C) to inhibit the growth of microorganisms.
Refrigeration units for compressor-condenser units (CCU). This is the "heart" of any industrial system, the source of cold. Large enterprises, such as the modernized poultry farm, use semi-hermetic or screw compressors that are integrated into a single system with cooling towers or air condensers. The trend is towards solutions using eco-friendly refrigerants with high energy efficiency, which reduces operating costs.
Thus, Agroforce's investments are not only about increasing the production of chicken products, but also about making a significant technological upgrade that will stimulate the market for high-tech industrial refrigeration equipment. The implementation of these systems will ensure the necessary level of quality, safety, and efficiency for the new "Important Chicken" line and strengthen the company's position in the competitive environment.
In December 2025, Copeland—a global leader in compressor manufacturing—unveiled a new development: a CO₂ scroll compressor featuring Dynamic Vapor Injection (DVI) technology. This milestone marked a significant step in the evolution of industrial refrigeration equipment, as the combination of the natural refrigerant CO₂ and an advanced vapor injection system opens up new possibilities for enhancing energy efficiency, reducing operating costs, and meeting environmental regulations.
 Выберите размер контейнера: Температурный режим: Новый или Б/У: | Прайс-лист на рефрижераторные контейнеры Вы выбрали: 40 футовые, низкотемпературные, новые 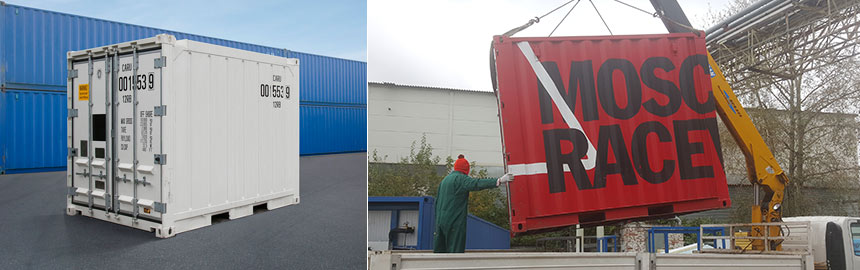
| ||||||||||||||||||||||||||||||||||||||||||||||||||||


 Telegram